China Hard Endoscope Cleaning Brush Manufacturer Quality Control Insights
2026-09-07
When a hard endoscope cleaning brush fails, it's rarely dramatic—just a missed speck of debris that could compromise the next procedure. That's why quality control in brush manufacturing is less about inspection and more about obsession. At KLDZS, a China-based manufacturer, we've learned that the smallest details—bristle density, shaft torque, tip adhesion—separate a brush that cleans from one that merely wipes. In this post, we share the behind-the-scenes QC insights most buyers never ask about, and why they matter more than the price tag.
Bristle Pull-Force Testing: The Overlooked Durability Metric
Most brush manufacturers obsess over bristle stiffness, density, and chemical resistance, yet rarely measure how firmly those fibers stay anchored. Bristle pull-force testing records the exact amount of tension needed to yank a single filament free from its base material. The process sounds straightforward: clamp a bristle, pull steadily, and log the peak load. But that simple number reveals a lot about adhesive bonding, mold design, and long-term structural integrity. Without it, a brush might feel great on day one and shed like a nervous dog by week three.
The metric matters most in high-contact environments, think industrial scrubbers, medical cleaning devices, or paint brushes used on rough surfaces. Each bristle experiences repeated micro-tugs during normal use. If the pull-force threshold dips below the friction generated by the target surface, shedding accelerates. Worse, loose bristles can contaminate products, scratch finishes, or end up where they shouldn't. Yet many quality-control checklists skip this test entirely, relying instead on visual inspection or a quick hand-pluck that varies wildly between operators.
Part of the neglect comes from a lack of universal standards. Unlike tensile strength or abrasion resistance, pull-force test results often depend on chuck type, pull speed, and ambient humidity. That makes cross-vendor comparison messy. Some forward-thinking teams now build custom fixtures and run statistical process control on pull-force data, catching adhesive batch problems before they hit the assembly line. For brushes sold on durability claims, ignoring this measurement is like rating a tire without checking bead retention.
Why Batch-Level Bioburden Sampling Beats Random Spot Checks
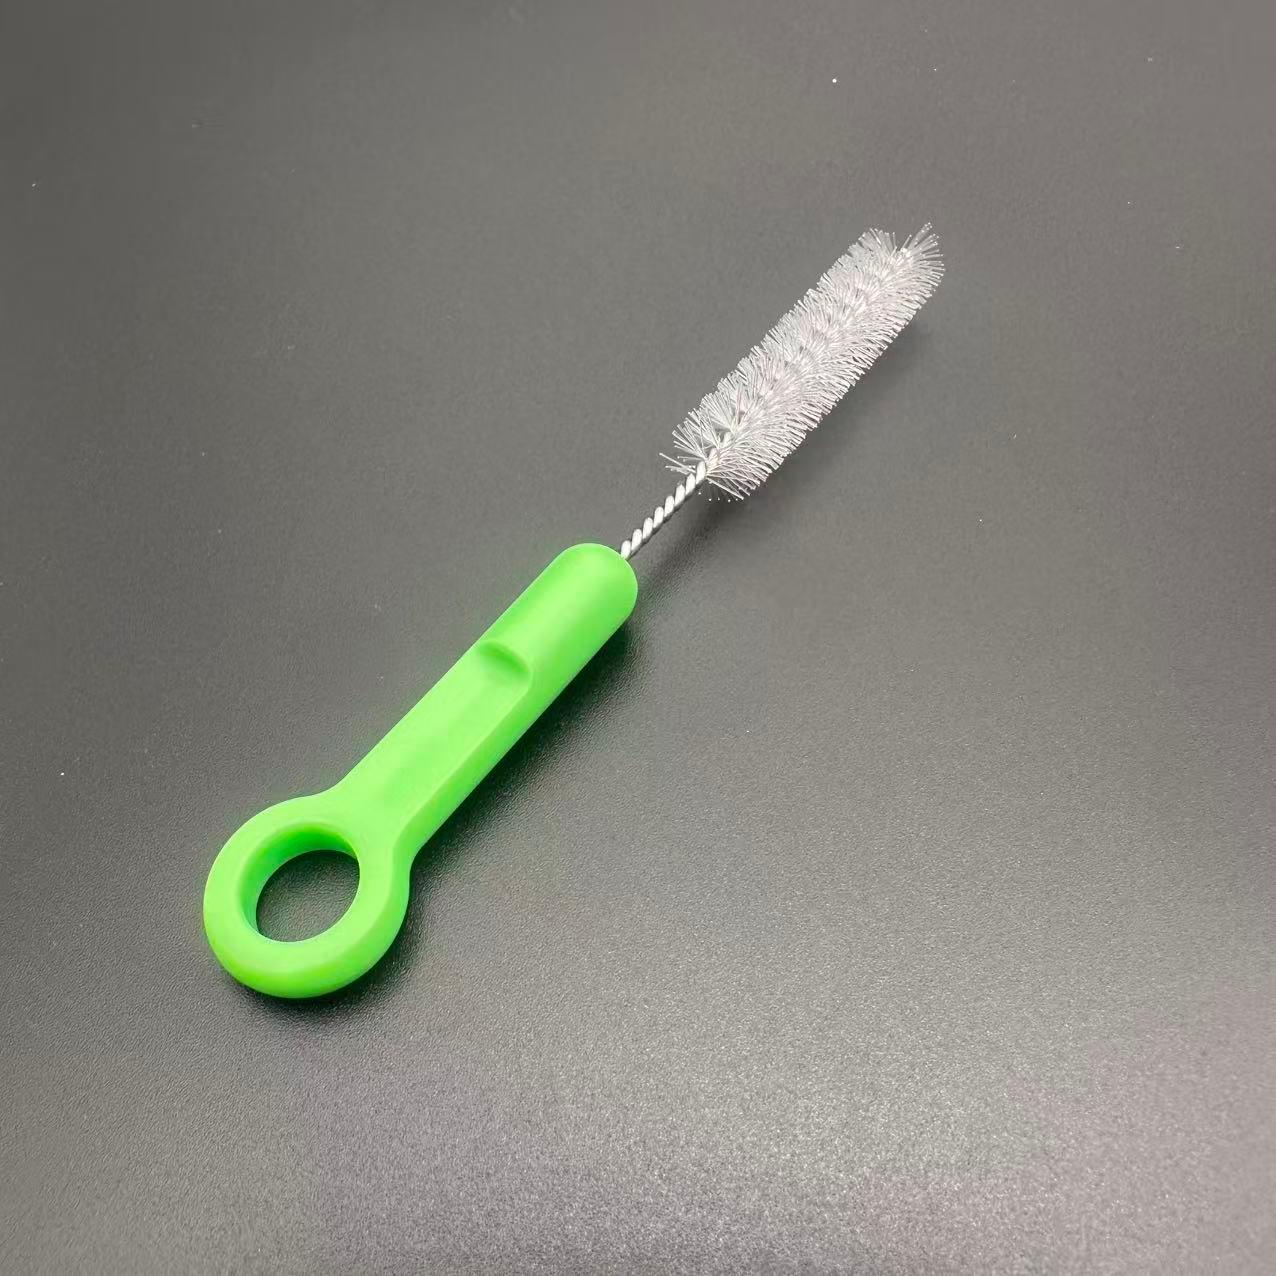
Random spot checks create a false sense of control. A single swab from a high-traffic area might miss contamination hiding in a corner, on a gasket, or inside a connector that only becomes problematic under specific process conditions. Because microbial distribution across a production batch is rarely uniform, relying on isolated locations means you’re often testing luck rather than cleanliness. Batch-level bioburden sampling, by contrast, pulls together multiple samples or composite aliquots that reflect the entire manufacturing run. This approach gives you a clearer picture of what actually accumulated during production, not just what happened to be on one surface at one moment.
Another advantage shows up when something goes wrong. If a random spot check fails, you know a small area was contaminated, but you have little idea whether the rest of that lot shares the same problem. With batch-level data, a positive result can be traced to a specific production cycle, raw material lot, or equipment setup, which makes corrective action far less speculative. It also reduces the temptation to over-clean a single “hotspot” while ignoring systemic issues that affect the whole batch.
From a quality assurance standpoint, batch-level bioburden sampling aligns better with how modern manufacturing actually operates. Processes run in defined lots, materials arrive in lots, and deviations are investigated by lot. Spot checks might catch gross failures, but they rarely detect low-level or intermittent contamination that builds up over an eight-hour shift. Batch-level monitoring turns microbial control from a game of hide-and-seek into a measurable parameter you can trend, tighten, and defend in an audit.
Cleanroom Assembly Lines Built Around Reusable Scope Compatibility
Cleanroom assembly for reusable endoscopes starts with the assumption that every major subassembly may return to the line for reprocessing, not just be built once. Workstations are positioned to keep contaminated incoming parts isolated from sterile outgoing trays, using split corridors and HEPA-filtered pass-throughs. The conveyor path is intentionally non-linear, allowing a scope body, insertion tube, or control handle to be pulled aside for leak testing or steam sterilization without disrupting the adjacent build sequence.
Tooling and fixtures are selected for repeated autoclave exposure rather than convenience. Sealed stainless steel frames, silicone-free clamps, and quick-change nest blocks let operators mount different scope diameters and bending section lengths without introducing particle-shedding plastics. Assembly aids such as torque drivers and fiber optic alignment jigs are stored in peel-pack pouches, so they can be sterilized alongside the reusable components they touch. This keeps material compatibility consistent across the entire line.
Each cleanroom zone logs reprocessing cycles, not just production counts. A handle that has gone through twelve steam cycles needs different seal seating pressure than a fresh one, so stations read a barcode or RFID tag on the subassembly and adjust assembly parameters automatically. Final packaging then verifies that the scope can survive the hospital's own sterilization protocol, with dry-time checks and channel patency tests performed before the reusable device leaves the controlled environment.
Packaging That Survives Gamma Irradiation Without Seal Fatigue
Medical device manufacturers face a persistent challenge: sterilizing sealed packages with gamma radiation without compromising the integrity of heat-sealed joints. Repeated exposure to ionizing radiation can cause polymer chains in sealant layers to cross-link or scission, leading to brittleness, micro-cracks, and eventual seal fatigue. This failure mode often appears only after weeks of storage, making it a silent threat to sterility assurance. Packaging engineers now turn to multi-layer films that combine radiation-resistant outer layers with elastomeric sealants, such as modified polyolefins or thermoplastic vulcanizates, which retain flexibility after doses up to 50 kGy.
The key lies in balancing seal strength with elongation at break. Traditional polyethylene seals, while strong initially, lose ductility under gamma exposure because free radicals attack the amorphous regions. By contrast, blends containing styrene-butadiene block copolymers or metallocene-catalyzed plastomers show a remarkable ability to dissipate radiation energy without forming stress concentrators at the seal interface. Coupled with optimized sealing parameters—lower dwell temperatures and longer pressure cycles—these materials produce seals that maintain peel strength above 1.5 N/15 mm even after double sterilization cycles.
Beyond material selection, package geometry plays a subtle but critical role. Sharp corners and tight folding points act as radiation dose amplifiers, creating localized hot spots that accelerate seal degradation. Designers mitigate this by rounding tray corners, using wider seal areas near notches, and avoiding excessive film tension during form-fill-seal operations. Accelerated aging tests, where sealed packages are irradiated at 40 kGy then subjected to 60°C for 30 days, now serve as a de facto benchmark for seal fatigue resistance. Only systems that show negligible change in burst pressure and dye penetration after such trials are considered viable for gamma-sterilized product lines.
How Factory Audits Keep Monofilament Diameter Within 0.02 mm
Precision doesn't happen by accident on a monofilament extrusion line. When the tolerance is just 0.02 mm, a single worn die or a subtle shift in cooling water temperature can push product out of spec within minutes. Factory audits target these variables directly, inspecting not only the laser micrometers mounted at each spinning station but also the frequency of their calibration against certified gauge blocks. Auditors compare recorded diameter readings against physical samples pulled from the line, looking for drift that automated systems might average away.
Beyond the measurement tools, a rigorous audit traces the process controls that hold diameter steady: melt pump RPM stability, quench bath turbulence, and tension feedback on the winders. Operators are interviewed about their response when an alarm signals a trend toward the upper or lower limit. Checklists verify that corrective actions are documented and retested, not just acknowledged. The best audits also examine the raw resin lot-to-lot viscosity data, since even perfect downstream control cannot fully compensate for upstream variation. All of this creates a paper trail showing that 0.02 mm isn't a marketing claim but a measured, repeatable outcome on every spool that leaves the floor.
Field Failure Data Driving Next-Generation Brush Head Design
When brush heads come back from the field with cracked necks, uneven bristle wear, or snapped retention clips, the patterns tell a story that lab simulations often miss. Every returned unit carries a timestamp, a usage environment, and sometimes a maintenance history that together reveal how real-world stress diverges from accelerated test profiles. Instead of treating these returns as isolated defects, design teams are now mapping them across production batches and customer segments to spot recurring failure modes early.
The analysis digs into material fatigue at the pivot joints, bristle tuft loss under abrasive cleaning agents, and thermal cycling effects from repeated autoclave exposure. By correlating failure rates with specific torque loads and brush head geometries, engineers can pinpoint which design features are weakest under actual brushing habits—like excessive lateral force near the gumline or repeated drops onto hard bathroom floors. This approach moves beyond generic durability scores and focuses on the exact stresses that shorten a brush head's service life in daily use.
Those findings directly shape the next generation of brush head architecture. For example, when field data shows that most neck fractures originate at a sharp internal radius, the new design incorporates a wider fillet and a reinforced overmold without adding bulk. If bristle splaying concentrates on the outer rows, the tufting pattern is rebalanced and the filament anchoring depth adjusted. The result is a brush head that doesn't just survive a standardized bench test, but holds up under the messy, unpredictable conditions where it actually gets used.
FAQ
Most factories run a three-stage visual check under bright LED light after molding and again after bristle insertion. They look for uneven tuft density, bent or missing bristles, and any rough seams on the handle that could scratch a scope channel. Some also run a pull-force test on a sample batch to confirm bristles won't shed during use.
They use precision-machined gauges that mimic the exact channel diameters specified by scope brands. Each production lot gets a go/no-go insertion test where the brush must pass through smoothly with moderate resistance. If the brush tip catches or bends a gauge wire, the whole lot gets reworked.
Suppliers of stainless steel wire and nylon bristles must provide mill certificates, but good manufacturers also do in-house hardness testing on the wire and a bend-cycle test on a small bristle sample. This catches batches that are too brittle or too soft before they reach the assembly line.
Yes, many run soak tests by immersing finished brushes in common enzymatic cleaners and high-level disinfectants for 24 to 72 hours, then checking for discoloration, swelling, or loss of bristle stiffness. Some also simulate repeated sterilization cycles in an autoclave tray to ensure the handle doesn't crack or warp.
Reputable factories laser-mark each brush handle with a batch code that links back to raw material lots, production date, shift, and the operator who performed the final inspection. This lets them isolate any field complaint to a specific day or even a specific machine within hours.
A specialized tensile tester grips a single tuft and pulls perpendicular to the brush axis. For endoscope brushes, a common acceptance criterion is no tuft loss below 15 Newtons force, and the brush must not show any exposed wire core after the test. Some buyers request 20 Newtons for longer brushes used in colonoscopes.
One notable practice is a 100% functional test on every brush rather than relying on AQL sampling. Workers manually insert each brush into a curved simulated channel template to feel for binding or excessive friction. This adds labor cost but catches subtle issues that automated vision systems might miss, because a brush can look perfect yet still feel too stiff in a bend.
Request the full in-process inspection report for a recent production lot, including photos of the gauge tests, pull-force data, and the signed sign-off from the QC supervisor. Also ask for a copy of their internal nonconformance log for the past three months—that shows whether they actually record and correct problems instead of hiding them.
Conclusion
Most quality conversations around hard endoscope cleaning brushes stall at bristle material or overall length, yet the real durability signal sits in bristle pull-force testing. Without a defined minimum extraction resistance, brushes shed filaments inside delicate channels during reprocessing—something that rarely shows up in standard visual checks. Chinese manufacturers who treat this as a first-line metric run destructive tests on every bristle lot and tie the results directly to brush head assembly. They also lean on batch-level bioburden sampling instead of scattered spot checks, pulling entire production lots for incubation rather than a single convenient swab. That approach catches contamination patterns tied to a specific shift, raw material batch, or cleanroom event. And these lines are not generic; they are built around reusable scope compatibility, with fixtures matching actual working channel diameters and bending radii so a brush passes through a scope model rather than a straight tube.
Packaging gets overlooked until a sealed pouch fails after gamma irradiation. A meaningful QC program cycles packaging through irradiation doses that mimic real distribution, then tests seal strength and integrity for fatigue, not just initial peel. Monofilament diameter control is another quiet battleground—factory audits verify that in-line laser measurement holds filament diameter within 0.02 mm across the entire spool, because even small drift changes brushing pressure and channel contact. Finally, smart manufacturers close the loop with field failure data. Returned brushes, customer complaints, and reprocessing department feedback feed directly into next-generation head design, so tweaks to distal tip geometry or bristle density come from actual clinical-use failures instead of bench assumptions. That feedback loop separates commodity suppliers from those genuinely improving scope cleaning outcomes.
Contact Us
Contact Person: Caiju Zhang
Email: [email protected]
Tel/WhatsApp: +86 14763963294
Website: https://www.kldbrush.com